Introduction
Hybrid organic-inorganic perovskite solar cells are heavily researched due to their potential to offer both high conversion efficiency and low cost. However, so far, environmental device stability is a major issue. Many avenues to improve the stability of these cells are being investigated with the added constraint of retaining or reaching a high efficiency. One avenue that is seen as very promising is the use of inorganic thin films in the design of the device. ALD with its excellent control of film growth and high-quality films is seen as a key technology to this end. Mostly for research but also for pilot-production, there is a desire for flexible tools with wide processing range and both plasma and thermal capabilities. Oxford Instruments FlexAL® and OpAL® tools are ideally suited in this respect. The goal of this white paper is to give a practical overview on what ALD is and how it can be used to benefit perovskite solar cells. To illustrate these benefits we will refer to some recent publications where Oxford Instruments equipment is utilised.
Atomic Layer Deposition
In atomic layer deposition (ALD), thin films are built up in cycles in which the surface is exposed to various vapor- or gas-phase species in alternating, separated doses. In each cycle, a submonolayer of material is deposited. As illustrated in Fig. 1, a typical cycle consists of four steps: (i) a precursor dosing step, where a precursor is typically an inorganic metal-organic or metal-halide (e.g. TMA); (ii) a purge and/or pump step; (iii) a co-reactant step, typically involving a small molecule (e.g. H2O or O2 plasma); and (iv) a purge and/or pump step. For the precursor, the element to be deposited is in many cases the metal center (e.g. Al), while for the reactant, it is typically a non-metal such as O. Together these then form the resulting film (e.g. Al2O3). For ALD, it is vital that the precursor and co-reactants react with the surface in a self-limiting way. The precursor molecules and co-reactants react neither with themselves nor with the surface groups that they create. In the purge and/or pump steps, the gaseous reaction products that may be generated during the surface reactions, as well as any excess precursor or co-reactant molecules, are removed from the ALD reactor. This is necessary to avoid reactions between precursor and co-reactant molecules directly in the gas phase or on the surface, as this could lead to an undesired chemical vapour deposition (CVD) component.
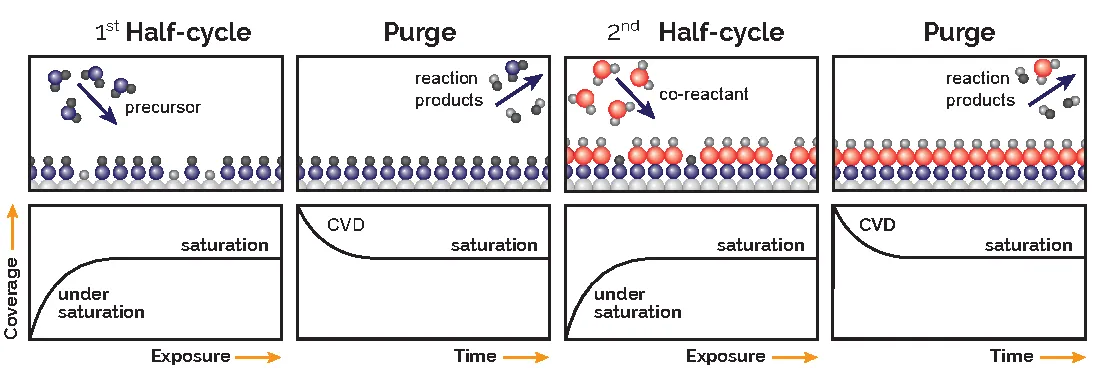
Fig. 1 — A schematic representation of the various steps in an ALD cycle consisting of two half-reactions. The exposures in the first half-cycle (precursor) and second half-cycle (co-reactant) are self-limiting such that the process stops when all available surface sites are occupied. The two half-cycles are separated by purge steps. The lower panels show the resulting coverage, or growth per cycle, as a function of exposure or time for that particular step. For sufficient exposure, saturated growth is obtained, while insufficient exposure results in incomplete saturation. For insufficient purging, a CVD component from mixing of the precursor and co-reactant is obtained.
ALD can provide the following benefits: precise thickness control; conformal coating even in high aspect ratio structures; low pin hole levels (i.e. no gas phase reactions generating particles); very thin and dense films (due to relatively low deposition rates compared to CVD and physical vapour deposition (PVD), typically 1 Å/cycle); wide variety of materials possible; and choice of deposition temperature down to low substrate temperatures (i.e. when using plasma). Fig. 2 illustrates the metrics that are important for covering a substrate with 3D features.
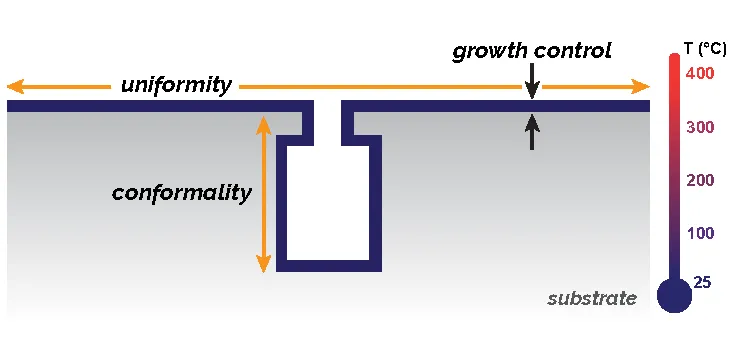
Fig. 2 — The coverage metrics of a film on a substrate with 3D features. Coverage of the planar surface is evaluated using the uniformity while the coverage of 3D features is evaluated using the conformality. The growth control over the film thickness itself is another important metric. The ability to achieve these metrics at low temperatures is an additional important aspect.
Thermal and Plasma ALD
H2O is the most reported oxygen source for metal oxide ALD. However, as H2O adsorbs strongly to surfaces it is difficult to purge from the reactor particularly at very low deposition temperatures (e.g. at 100°C and below). H2O is also often not sufficiently reactive at low temperatures to result in film deposition. Similarly NH3 for the growth of nitrides can be used, but can be difficult to purge and insufficiently reactive. In order to increase reactivity, species with relatively short lifetimes can be used such as plasma species. In the case of ALD using plasmas, the plasma species are generated close to or in the reaction chamber. When employing a plasma, various highly reactive species can contribute to the surface chemistry, such as radicals and ions. Radio-frequency power is used to dissociate the source gas (e.g. O2) into plasma species (e.g. O2, O+ ions and electrons). In the case of a remote plasma (as is used in Oxford Instruments Plasma Technology ALD systems), both radicals and ions can be present, and their levels can be tuned by changing the plasma power and pressure. At low plasma power and high pressure the ion energy and flux reduces to negligible levels and radicals are the main species (e.g. O atoms in an O2 plasma or H atoms in an H2 plasma). To have the highest reactivity, the plasma can be operated at high power and low pressure to have the highest radical densities and also moderate ion energies. These conditions are beneficial for the growth of conductive nitrides such as TiN. Processes using a plasma are often referred to as "plasma ALD" while processes not using plasma are in that context referred to as "thermal ALD".
The following benefits can be present for plasma ALD processes: improved material properties (i.e. film density and composition can be influenced and lower impurities can be obtained); increased choice of precursors and materials; reduction of the needed substrate temperatures; possibility of surface pre-treatment (e.g. surface activation and surface cleaning); increased growth rate; and shorter nucleation periods (some thermal ALD process can have a growth delay when nucleating on certain materials).
Oxford Instruments FlexAL and OpAL ALD Tools
The following requirements are important for an ALD reactor. Firstly, the reactor heats the samples to the desired deposition temperature. Secondly, pulses of precursors and co-reactants need to be injected into the reactor volume, and an inert gas is often used to purge the reactor volume between these steps. Generally, the reactor volume is continuously pumped to achieve a certain pressure (e.g. 80 mTorr). These reactor requirements dictate the design. Most ALD reactor designs are derived from CVD reactors. However, contrary to CVD, ALD is not a continuous process and therefore the reactor volume has to be filled and purged efficiently to achieve reasonable cycle times. Furthermore, the pulsing of the precursor and co-reactant has to be automated with accurate timing. For plasma ALD, the co-reactants are species with a limited lifetime, which requires the integration of equipment that generates the species relatively close to the substrate. Fig. 3 shows a schematic and explanation of the Oxford Instruments FlexAL ALD tool. Our OpAL tool has a similar design but is an open-load system without a turbopump and automatic pressure control (APC). Both are cutting edge plasma ALD systems with thermal ALD as standard. Plasma and thermal ALD cycles can be used within a single recipe and no hardware changes are required to switch mode between plasma and thermal ALD (e.g. start with thermal Al2O3 on sensitive interface but continue with plasma ALD for best material properties).
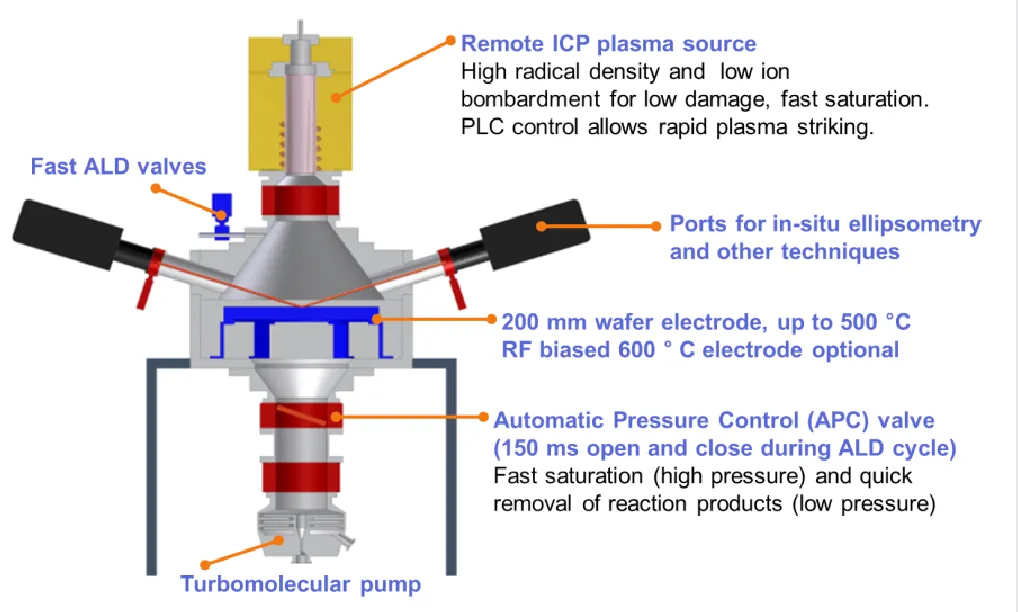
Fig. 3 — Schematic of the FlexAL ALD system. The key components are indicated as well as some of their benefits.
Compared to thermal CVD, thermal ALD can typically achieve good material properties at lower deposition temperatures (200 – 400°C). However, at even lower temperatures (25 - 100°C), thermal ALD processes can have low material purity, low growth rates or long cycle times. Plasma ALD can generally be used at lower temperatures because of its higher reactivity. Using plasma ALD, several oxides such as Al2O3, TiO2 and SiO2 have been deposited down to room temperature.
Perovskite Solar Cells
A perovskite solar cell is a type of solar cell which includes a perovskite structured compound such as a hybrid organic-inorganic lead halide-based material, as the light-harvesting active layer. Perovskite materials such as methylammonium lead halides are inexpensive to produce and simple to manufacture. Solar cell efficiencies of devices using these materials have increased from 3.8% in 2009 to 22.7% in late 2017, making this the fastest-advancing solar technology to date. With the potential of achieving even higher efficiencies and the very low production costs, perovskite solar cells have experienced intensive research. Furthermore, perovskite solar cells are the only thin film solar cell technology with enough current and band gap control to be combined in a tandem structure with c-Si solar cells. However, so far perovskite solar cells are only the size of a fingernail and degrade quickly in moist environments. Only recently, somewhat larger lab-scale mini-modules have been demonstrated.
Perovskite devices are usually fabricated using solution based processing, and the resulting organo-lead mixed absorber layer is sensitive to high temperature. For instance, exposure of the perovskite to a temperature of 100°C can result in layer damage with long exposure times. The need for low temperature processing is one potential advantage of plasma ALD for these devices.
How ALD Can Benefit Perovskite Solar Cells
Both plasma and thermal ALD offer benefits to perovskite solar cell production and this section illustrates a few examples to explain how certain merits of ALD can be implemented. ALD film characteristics of having: low pinhole levels, low temperature deposition, high material quality, excellent process control and interface engineering are envisaged to be extremely advantageous to perovskite solar cells.
As previously mentioned, perovskite devices are known to be highly susceptible to deterioration. This has been linked to both extrinsic factors (i.e. oxygen, light, moisture and temperature) and intrinsic factors (i.e. device interfaces and species diffusion). To limit the effect of oxygen and moisture on the device, moisture barriers can be used. ALD is known to provide excellent moisture barrier properties which are also promising for perovskite solar cells. A wide range of barrier materials can be used where low temperature plasma ALD of Al2O3 and low temperature plasma ALD of SiNx have shown excellent results.
The instability of perovskites is mostly attributed to intrinsic factors (e.g. deterioration of device interfaces and species diffusion). Fig. 4 shows the comparison in solar cell efficiency for cells with and without thermal ALD Al2O3 directly deposited on the perovskite absorber layer before finishing the device. This optimum is achieved with just 10 ALD cycles, where a thicker layer of Al2O3 is too insulating to have good hole current extraction. Note that in our tools low partial pressures of water can be used in the ALD process which is not detrimental for the perovskite layer used in this study.
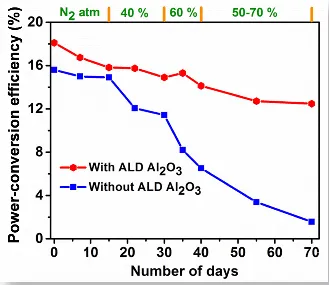
Fig. 4 — Improved efficiency and stability by thermal ALD Al2O3 on OpAL as demonstrated by the efficiency of perovskite devices with and without ALD Al2O3 as a function of storage time under varied humidity conditions (see labels top axis).Opening opportunities for the adoption of thermal ALD processes directly on the perovskite layer. A single water dose in our tools can increase the relative humidity to 0.1% which is much lower than the device experiences in ambient environment. So far, this is the only case of direct ALD on the perovskite layer that led to high efficiency cells.
Besides protective layers, a large part of the research aimed at improving the intrinsic stability of perovskite solar cells revolves around inorganic carrier transport layers (typically organic layers are used in perovskite devices). These layers should be blocking for one carrier (e.g. holes) and conductive for another (e.g. electrons), in the resulting band diagram of the solar cell device. For blocking purposes and good dielectric properties plasma ALD has a benefit because of high material quality and low pinhole levels and TiO2 plasma ALD has been demonstrated to perform well. Fig. 5 shows a future concept stack where the Pb containing layer shows the position of the perovskite material and stacks of plasma ALD TiO2 and MoO3 are indicated.
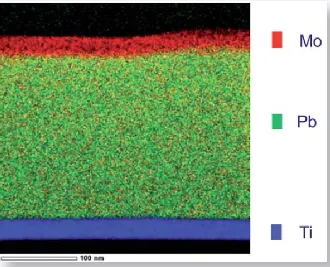
Fig. 5. TEM image with elemental mapping acquired using Energy Dispersive Spectroscopy (EDS) of future concept of a perovskite (methylammonium lead iodide) film sandwiched between two plasmaassisted ALD layers deposited using the OpAL tool. The Pb containing layer shows the position of the perovskite material and the Ti and Mo indicate the inorganic carrier transport layers. 25 nm of TiO2 was deposited at 150°C and the 20 nm of MoO3 on top was deposited at 50°C.
If direct exposure to O2 plasma needs to be avoided, other plasmas can be used (e.g. N2 or H2) which have been demonstrated to not damage power semiconductor devices during processing. N2 plasma and subsequent exposure to H2O should result in oxide material while the N2 plasma might keep the nitrogen levels of the perovskite intact. Alternatively, a thin thermal ALD layer can be deposited (e.g. the process with 10 cycles of Al2O3 described in the previous section). No hardware change is needed in our tools to switch between thermal and plasma ALD. Both plasma and thermal ALD can easily be combined and a few ALD cycles are expected to have a strong protective effect. Although this holds for Al2O3, it might not be true for all thermal processes and a nucleation delay or a chemical interaction can be a concern on the surface of the perovskite material. For instance thermal ALD of ZnO did not lead to growth but to chemical etching of the perovskite. In this case, a plasma treatment or a Al2O3 interlayer might be beneficial. In general, rapid processing will be essential to allow for minimal thermal budgets since prolonged exposure to 100°C can damage the perovskite material. Furthermore the main application of ALD for perovskite solar cells might not be on the perovskite directly but at other interfaces in the device.
Many materials and functional layers can be deposited by ALD: n-type electron-transport layer metal oxides (e.g. TiO2, SnO2, ZnO), passivation layers with ultra-thin (3–6 nm) TiO2 films or sub-nanometre Al2O3 layers, hole-transport layers such as p-type metal oxides (e.g. NiO) or high-work-function metal oxides (MoO3), and furthermore wide band gap (e.g. Ga2O3, HfO2) metal oxides and tunnel junctions or interface layers. Established processes or starting recipes are available for all these materials from Oxford Instruments.
For indoor energy harvesting to enable indoor wireless sensors and devices, perovskite solar cells are also considered. In this environment, decent efficiency at low light levels is required but generally solar cell efficiency is determined at daylight sun levels (i.e. 2-3 orders of magnitude more light). Loss of carriers is much more apparent at these low light levels and to obtain a high efficiency an ALD blocking layer with low pinhole levels was found to be beneficial. At 400 lux an efficiency of 12.1% was obtained for a flexible perovskite solar cell using an 11-nm plasma ALD TiO2 compact blocking layer on PET/ITO substrates, which outperforms other flexible solar cell techniques such as a-Si, dye sensitized, organic, and CIGS under the same test conditions.
ALD TiO2 can also be used as the electron transport layer in thin film perovskite solar cells even though the band alignment is not ideal. In this case a short CF4 plasma treatment has been found to beneficially alter the conduction band alignment between the perovskite and TiO2 and also improve adhesion. This work was done on a barrel etcher, but should be possible using an Oxford Instruments ICP etcher.
Conclusion and Outlook
Making perovskite solar cells both stable and with high efficiency is a challenge but techniques such as ALD have the ideal characteristics to work towards this exciting goal. Key aspects are the resulting low pinhole levels, which are essential for moisture barriers and blocking layers. The capability of low temperature deposition is crucial for processing on the top surface of the perovskite device where the thermal budget is limited. In general to allow low defect devices and interfaces, ALD's high material quality, excellent process control, and ability for interface engineering are envisaged to be a big benefit.
In addition to ALD, other nanoscale or atomic scale processes could be beneficial for perovskite solar cells. Etching of undesired crystal orientations or etching away defects could be an option. Band position tuning by plasma treatments/doping but also other gas-phase chemical treatments could be of interest. 2D materials are not expected to be of interest so far but other sulphides could be investigated. Understanding and control of sensitive interfaces as in many nanoscale applications will be essential and the range of Oxford Instruments techniques can be utilized to this end.
References
- H.C.M. Knoops, S.E. Potts, A.A. Bol, and W.M.M. Kessels, Handbook of Crystal Growth, 2nd edition, p. 1101–1134 (2015).
- V. Miikkulainen, M. Leskelä, M. Ritala, and R.L. Puurunen, J. Appl. Phys. 113, 21301 (2013).
- H.B. Profijt, S.E. Potts, W.M.M. Kessels, and M.C.M. Van de Sanden, J. Vac. Sci. Technol. A 29, 50801 (2011).
- S.E. Potts and W.M.M. Kessels, Coord. Chem. Rev. 257, 3254 (2013).
- M.D. Groner, F.H. Fabreguette, J.W. Elam, and S.M. George, Chem. Mater. 16, 639 (2004).
- S.E. Potts, H.B. Profijt, R. Roelofs, and W.M.M. Kessels, Chem. Vap. Depos. 19, 125 (2013).
- NREL, https://www.nrel.gov/pv/assets/images/efficiency (n.d.).
- F. Di Giacomo, V. Zardetto, A. D'Epifanio, S. Pescetelli, F. Matteocci, S. Razza, A. Di Carlo, S. Licoccia, W.M.M. Kessels, M. Creatore, and T.M. Brown, Adv. Energy Mater. 5, 1401808 (2015).
- V. Zardetto, B.L. Williams, A. Perrotta, F. Di Giacomo, M.A. Verheijen, R. Andriessen, W.M.M. Kessels, and M. Creatore, Sustain. Energy Fuels 1, 30 (2017).
- W. Keuning, P. van de Weijer, H. Lifka, W.M.M. Kessels, and M. Creatore, J. Vac. Sci. Technol. A. 30, 01A131 (2012).
- A.-M. Andringa, A. Perrotta, K. de Peuter, H.C.M. Knoops, W.M.M. Kessels, and M. Creatore, ACS Appl. Mater. Interfaces 27, 22525 (2015).
- D. Koushik, W.J.H. Verhees, Y. Kuang, S. Veenstra, D. Zhang, M.A. Verheijen, M. Creatore, and R.E.I. Schropp, Energy Environ. Sci. 10, 91 (2017).
- G. Lucarelli, F. Di Giacomo, V. Zardetto, M. Creatore, and T.M. Brown, Nano Res. 10, 2130 (2017).
- S. Huang, Q. Jiang, S. Yang, C. Zhou, and K.J. Chen, IEEE Electron Device Lett. 33, 516 (2012).
- A.J. Kerr, E. Chagarov, S. Gu, T. Kaufman-Osborn, S. Madisetti, J. Wu, P.M. Asbeck, S. Oktyabrsky, and A.C. Kummel, J. Chem. Phys. 141, 104702 (2014).
- J. Son, V. Chobpattana, B.M. McSkimming, and S. Stemmer, J. Vac. Sci. Technol. A Vacuum, Surfaces, Film. 33, 20602 (2015).
- V. Zardetto, F. di Giacomo, H. Lifka, M.A. Verheijen, C.H.L. Weijtens, L.E. Black, S. Veenstra, W.M.M. Kessels, R. Andriessen, and M. Creatore, Adv. Mater. Interfaces 5, 1701456 (2018).